Premium Hydrogen Cup Factories: Advanced Manufacturing for Hydrogen Water Technology

hydrogen cup factories

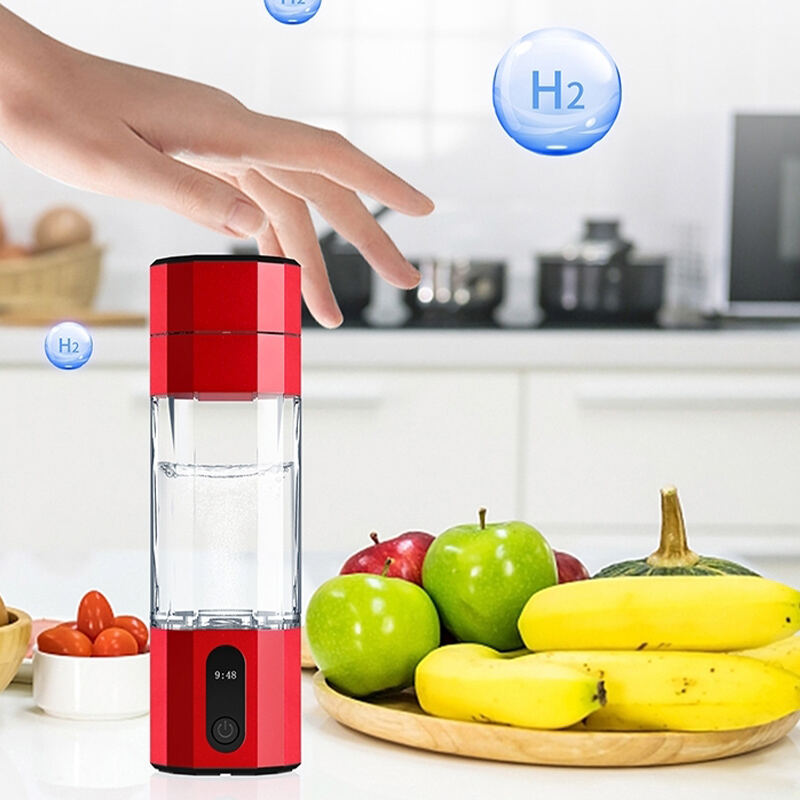
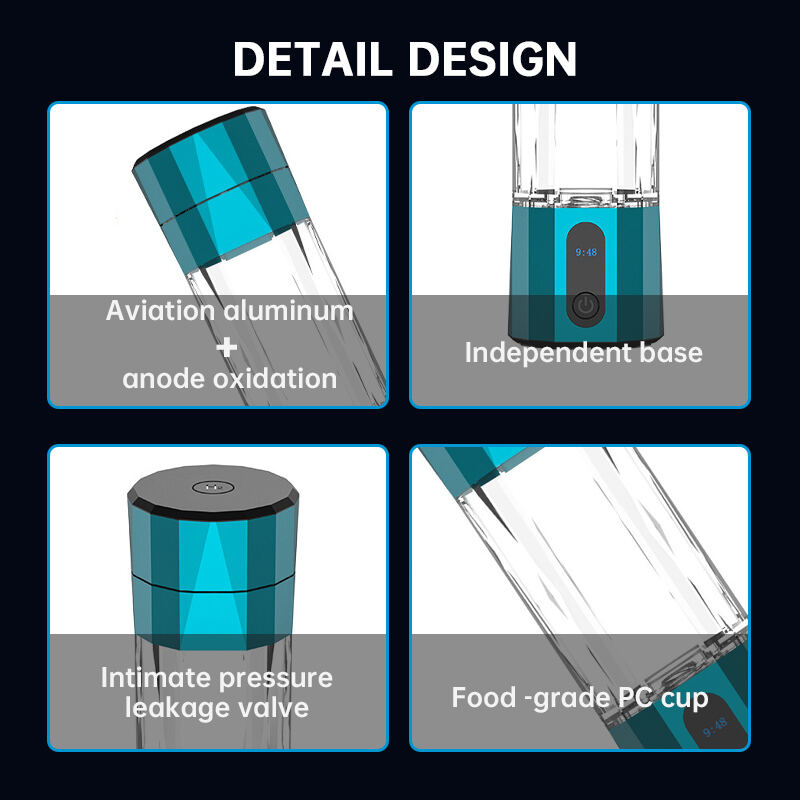
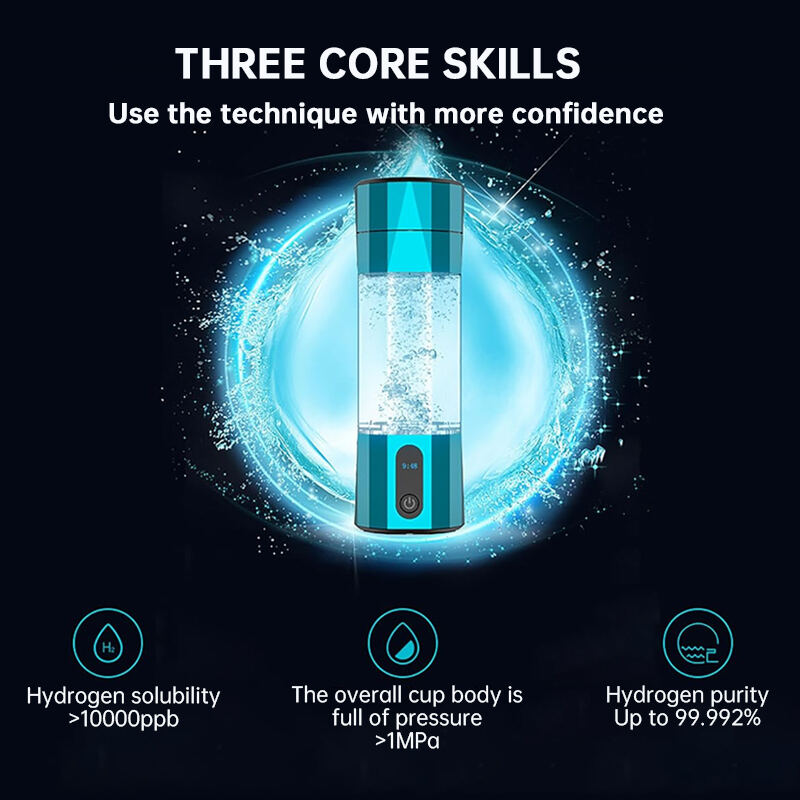
Hydrogen cup factories represent specialized manufacturing facilities dedicated to producing hydrogen-rich water containers that utilize advanced electrolysis technology. These production centers focus on creating portable devices designed to infuse regular drinking water with molecular hydrogen through sophisticated electrochemical processes. The primary function of hydrogen cup factories involves assembling components including electrolysis chambers, platinum-coated titanium electrodes, food-grade materials, and integrated power systems into consumer-ready products. Modern hydrogen cup factories employ precision engineering to ensure each unit meets strict quality standards for hydrogen concentration output, typically ranging from 800 to 1500 parts per billion. The technological infrastructure within these facilities encompasses automated assembly lines, quality control stations, material testing laboratories, and packaging departments. Production processes integrate multiple stages including electrode preparation, chamber assembly, electrical circuit installation, leak testing, and performance verification. Hydrogen cup factories source premium materials such as Tritan copolyester, borosilicate glass, and medical-grade silicone to ensure product safety and durability. The manufacturing environment maintains controlled conditions to prevent contamination and ensure consistent product quality. These facilities serve diverse market segments including health-conscious consumers, athletes, wellness centers, and retail distributors. Applications extend beyond personal use to include hospitality services, fitness facilities, and corporate wellness programs. The factories implement research and development divisions that continuously refine electrolysis efficiency, battery longevity, and user interface design. Production capacity varies significantly, with established hydrogen cup factories capable of manufacturing thousands of units daily. Quality assurance protocols include testing for hydrogen generation rates, battery cycle life, material safety certifications, and electromagnetic compatibility. The facilities also manage supply chain logistics, coordinating with component suppliers, packaging providers, and distribution networks to ensure timely product delivery to global markets.
New Product Releases

Hydrogen cup factories deliver substantial benefits that directly impact product quality, cost efficiency, and market accessibility for consumers seeking hydrogen-enriched water solutions. The centralized production model enables economies of scale, reducing per-unit manufacturing costs and making hydrogen water technology affordable for broader consumer demographics. By consolidating expertise and resources, these facilities achieve consistent quality standards that individual manufacturers cannot replicate, ensuring every product meets performance specifications. The specialized nature of hydrogen cup factories allows for continuous process optimization, where engineers refine production techniques to enhance hydrogen generation efficiency and extend product lifespan. This focused approach results in devices that produce higher hydrogen concentrations more reliably than earlier generation products. Customers benefit from rigorous testing protocols implemented throughout the manufacturing process, including material safety verification, electrical safety compliance, and performance consistency checks. The factories maintain relationships with certified suppliers, guaranteeing that components meet international safety standards for food contact materials and electrical devices. Production efficiency translates to faster market availability, allowing consumers to access the latest technological improvements without extended waiting periods. Hydrogen cup factories invest in automation technology that minimizes human error during assembly, resulting in products with lower defect rates and improved reliability. The concentrated expertise within these facilities fosters innovation, as engineers and technicians collaborate to solve technical challenges and develop enhanced features. Customers gain access to products incorporating the latest advancements in electrode design, battery technology, and user interface functionality. The manufacturing scale enables comprehensive warranty programs and customer support infrastructure, providing buyers with confidence in their purchase decisions. Environmental benefits emerge from optimized production processes that reduce material waste and energy consumption compared to distributed manufacturing models. The factories implement quality management systems that track each production batch, enabling rapid identification and resolution of any quality issues. This traceability ensures product recalls, if necessary, can be executed efficiently to protect consumer safety. The competitive environment among hydrogen cup factories drives continuous improvement in product features, pricing, and customer service. Bulk purchasing power allows these facilities to secure premium materials at competitive prices, passing savings to end consumers. The standardized production environment ensures compatibility with replacement parts and accessories, extending product utility over time. Training programs within hydrogen cup factories develop skilled workforces capable of maintaining high production standards and adapting to technological evolution. The established infrastructure supports rapid scaling to meet growing market demand without compromising quality standards.

Latest News

Minter: Revolutionizing Healthcare with Advanced Hydrogen Solutions & Wellness Gadgets

21

Aug

Minter: Revolutionizing Healthcare with Advanced Hydrogen Solutions & Wellness Gadgets

Minter, a pioneering force in the health tech industry, is dedicated to enhancing well-being through innovative products designed for modern lifestyles. Our core portfolio encompasses a range of cutting-edge healthcare solutions, including hydrogen i...
View More
Discover Minter - Your One-Stop Solution for Holistic Healthcare

21

Aug

Discover Minter - Your One-Stop Solution for Holistic Healthcare

Minter, a leading name in the healthcare industry, is dedicated to providing innovative and high-quality health care products that cater to your every need. Our main products include hydrogen inhaler, hydrogen water bottle, dental products, massage p...
View More
Unlock Health and Wellness with Minter's Innovative Products

30

Apr

Unlock Health and Wellness with Minter's Innovative Products

In today's fast-paced world, maintaining good health can be challenging. Minter understands this all too well, which is why we have dedicated ourselves to the development and distribution of a wide range of health care products. Our commitment to inn...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

hydrogen cup factories

Advanced Electrolysis Technology Integration

Advanced Electrolysis Technology Integration

Hydrogen cup factories distinguish themselves through sophisticated integration of electrolysis technology that transforms ordinary water into hydrogen-rich beverages with therapeutic potential. The manufacturing process centers on precision assembly of electrolysis chambers featuring platinum-coated titanium electrodes, which serve as the catalytic surface for water molecule separation. These factories invest heavily in electrode preparation techniques, including plasma coating processes that ensure uniform platinum distribution across titanium substrates, maximizing catalytic efficiency and longevity. The electrolysis chambers undergo meticulous design optimization to enhance hydrogen bubble formation and dissolution rates, incorporating features such as micro-porous diffusion membranes and optimized electrode spacing. Quality control systems within hydrogen cup factories test each electrolysis unit for hydrogen generation capacity, measuring output concentrations using specialized sensors to verify performance meets specifications of 1000 to 1500 parts per billion. The factories implement advanced power management circuits that regulate voltage and current delivery to electrodes, preventing overheating while maximizing hydrogen production efficiency. This technological sophistication ensures consistent performance across varying water quality conditions, including different mineral content and pH levels. Engineers within these facilities continuously research electrode materials and coating techniques to extend operational lifespan beyond 3000 cycles while maintaining peak performance. The integration process includes hermetic sealing technologies that prevent hydrogen escape and contamination ingress, preserving the purity of generated hydrogen gas. Hydrogen cup factories also incorporate safety mechanisms including automatic shutoff systems that activate when water levels drop below safe operating thresholds, protecting both the device and user. The technological infrastructure supports rapid prototyping of new designs, allowing factories to test innovations in electrode geometry, chamber configuration, and power delivery systems before full-scale production. This capability enables hydrogen cup factories to respond quickly to emerging research on optimal hydrogen concentrations for various health applications. The manufacturing precision ensures minimal variation between units, providing consumers with reliable performance regardless of production batch. Advanced testing equipment within these facilities measures dissolved hydrogen concentrations, oxidation-reduction potential, and pH levels to verify each unit meets stringent quality standards before packaging and distribution to global markets.
Comprehensive Quality Assurance Systems

Comprehensive Quality Assurance Systems

Hydrogen cup factories implement multi-layered quality assurance frameworks that guarantee product safety, performance consistency, and regulatory compliance across all manufacturing stages. The quality management infrastructure begins with incoming material inspection, where specialized laboratories test raw materials including plastics, glass, electrodes, and electronic components against international safety standards. These facilities maintain certification compliance with FDA food contact regulations, European Union material safety directives, and various national quality standards. Each production batch undergoes documented testing protocols that create traceable quality records, enabling rapid identification of any component or process variations that might affect final product performance. Hydrogen cup factories employ automated optical inspection systems that examine assembled units for physical defects, including cracks, misalignments, and surface imperfections that could compromise functionality or aesthetics. Electrical testing stations verify circuit integrity, battery charging performance, and power consumption characteristics to ensure devices operate within designed parameters. Performance validation includes extended operation tests where sample units from each production run generate hydrogen continuously for hours while sensors monitor output consistency and component temperature stability. The factories conduct accelerated aging tests that simulate months of regular use within compressed timeframes, identifying potential failure modes before products reach consumers. Material safety testing extends beyond initial certification to include batch testing for heavy metal content, plasticizer migration, and chemical stability under various temperature and pH conditions. Hydrogen cup factories maintain calibrated measurement equipment traceable to national standards, ensuring accuracy of all quality metrics including hydrogen concentration measurements, dimensional tolerances, and electrical specifications. The quality assurance teams document non-conformances and implement corrective action procedures that address root causes rather than symptoms, continuously improving manufacturing processes. Environmental testing chambers subject products to temperature extremes, humidity variations, and mechanical stress to verify durability under diverse usage conditions. Microbiological testing ensures materials resist bacterial colonization and remain hygienic throughout expected product lifespan. The comprehensive approach includes packaging integrity tests that confirm products remain protected during shipping and storage. Hydrogen cup factories also conduct user safety evaluations, testing for electrical shock hazards, chemical leaching, and mechanical failure risks. This rigorous quality framework provides consumers with confidence that purchased products will perform safely and effectively throughout their intended lifespan, backed by detailed quality documentation and responsive customer support systems.
Scalable Production and Market Responsiveness

Scalable Production and Market Responsiveness

Hydrogen cup factories demonstrate exceptional capability in scaling production volumes while maintaining quality standards, enabling rapid market expansion and competitive pricing strategies. The manufacturing infrastructure incorporates flexible assembly lines that can adjust output rates based on demand fluctuations without requiring extensive reconfiguration or quality compromises. This scalability stems from modular production station designs where individual workstations handle specific assembly tasks, allowing factories to add capacity by replicating proven station configurations. Automated material handling systems within hydrogen cup factories transport components between stations efficiently, minimizing production bottlenecks and reducing labor requirements. The facilities implement lean manufacturing principles that eliminate waste in material usage, production time, and energy consumption, translating to cost savings passed to consumers through competitive pricing. Inventory management systems coordinate component procurement with production schedules, ensuring continuous operation without excessive material stockpiling that ties up capital. Hydrogen cup factories maintain relationships with multiple suppliers for critical components, creating supply chain resilience that prevents production disruptions from single-source failures. The production flexibility enables rapid introduction of design improvements and new models without extensive retooling delays, keeping product offerings aligned with evolving consumer preferences and technological advancements. Market responsiveness extends to customization capabilities, where factories can produce private label versions, adjust color schemes, or modify packaging to meet specific retailer or distributor requirements. The scalable infrastructure supports both high-volume production for mass market distribution and smaller batch runs for specialized applications or regional market testing. Hydrogen cup factories utilize data analytics to forecast demand patterns, optimizing production planning to minimize inventory carrying costs while ensuring product availability. The manufacturing efficiency enables competitive pricing that makes hydrogen water technology accessible to broader consumer segments beyond early adopters and premium markets. Quality maintenance during scaling operations relies on standardized work procedures, comprehensive operator training programs, and statistical process control methods that detect variations before they affect product quality. The factories invest in automation technologies that handle repetitive tasks with consistent precision, freeing skilled workers to focus on quality verification and process improvement activities. Production capacity expansion can occur incrementally, allowing hydrogen cup factories to grow in alignment with market demand rather than requiring large capital investments that create excess capacity. This operational flexibility positions these facilities to capitalize on growing consumer interest in hydrogen water benefits while maintaining the quality standards that build brand reputation and customer loyalty in competitive wellness product markets.